Gripper System
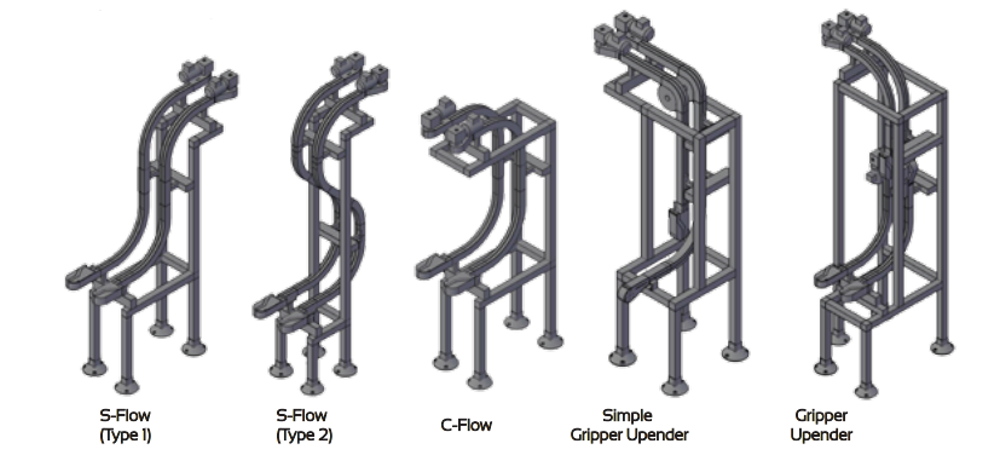
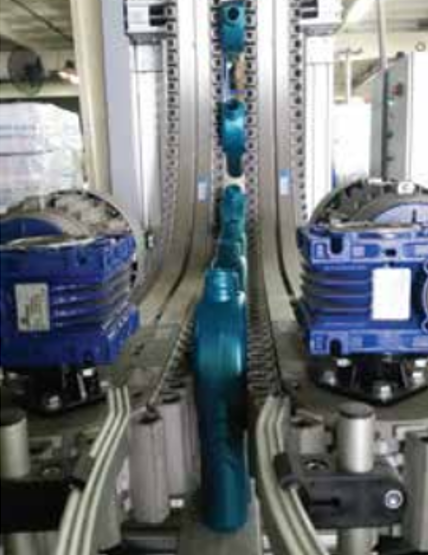
A gripper conveyor is a specialized material handling system that securely holds products between two synchronized side-gripping chains, allowing smooth transportation in horizontal, inclined, or vertical directions. It is ideal for applications requiring product elevation, inversion, orientation changes, or transfer between production processes while minimizing floor space.
Designed for flexibility and reliable performance, gripper conveyors integrate seamlessly with filling, packaging, labeling, inspection, and automated production lines. Their modular construction allows easy installation, quick product changeovers, and smooth handling of bottles, containers, cartons, and other packaged products.
Key Features
- Secure side-gripping system for stable product handling
- Vertical, inclined, and horizontal conveying
- Saves floor space through vertical transportation
- Creates overhead cooling and accumulation buffers
- Easy integration with filling, packaging, and processing lines
- Adjustable gripping system for fast product changeovers
- Smooth handling with minimal product damage
Technical Specifications
- Gripping System: Dual synchronized modular chains with adjustable gripper pads
- Frame: Aluminum or stainless steel construction
- Drive System: Electric gear motor with synchronized chain drive
- Speed Control: Fixed or variable speed (VFD)
- Customization: Width, height, length, and gripping range tailored to customer requirements
Applications
- Product elevation
- Product inversion (reverting)
- Product orientation change
- De-pucking systems
- Air rinser integration
- Food & beverage production
- Packaging and bottling lines
- Pharmaceutical and consumer goods industries