Overhead conveyor
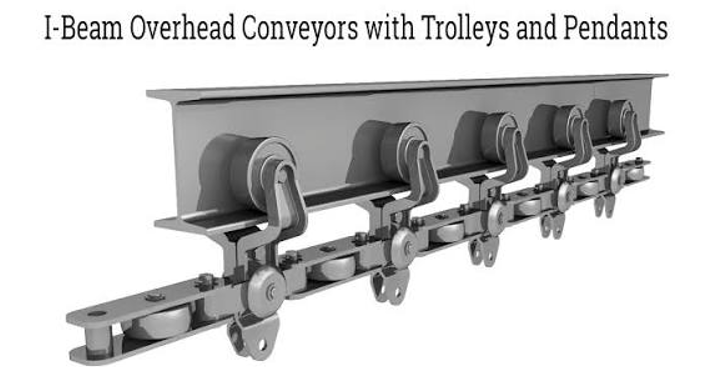
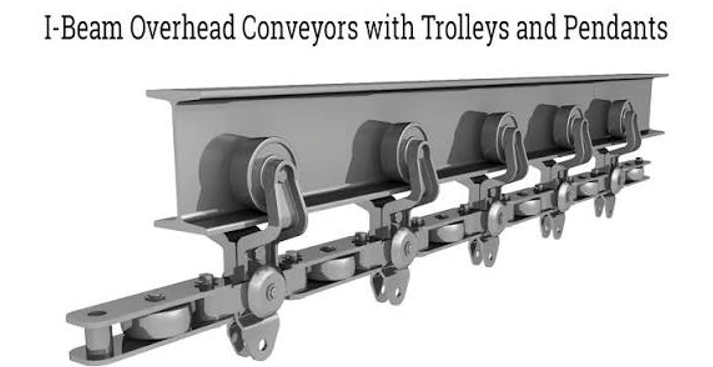
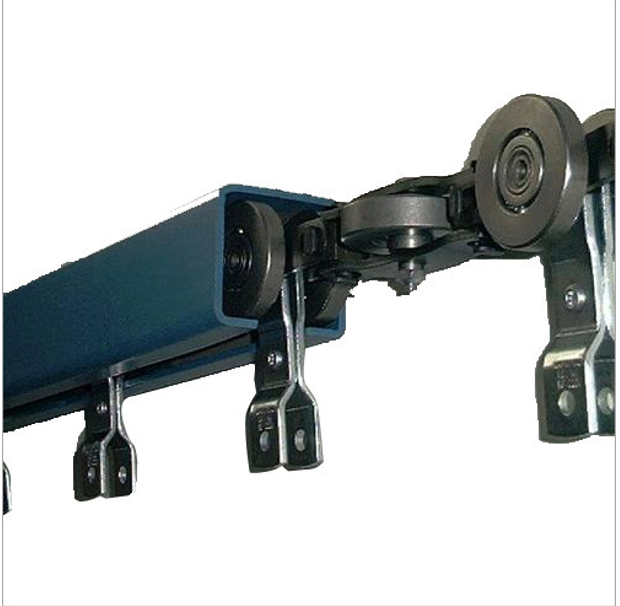
An overhead conveyor is a space-saving material handling system designed to transport products above the production floor, maximizing workspace while ensuring smooth, continuous product flow. Using a chain running inside an enclosed track with suspended carriers, it is ideal for moving products through assembly, painting, storage, inspection, and manufacturing processes.
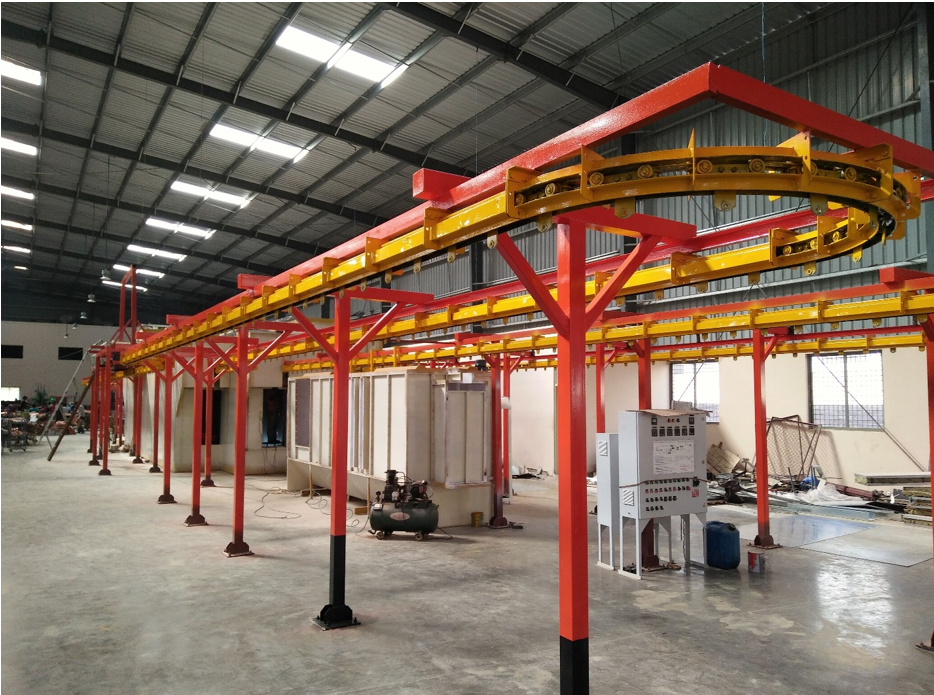
Its modular design allows straight sections, horizontal and vertical curves, elevation changes, and multi-floor layouts, making it adaptable to virtually any facility. Available in manual or powered configurations, overhead conveyors can handle light to heavy loads while reducing floor congestion and improving production efficiency.
Key Features
- Maximizes floor space with overhead transport
- Flexible layouts with straight, curved, and inclined tracks
- Manual or powered operation
- Smooth, reliable, and low-maintenance performance
- Modular design for easy expansion and automation
- Optional accumulation, transfer, and power busbar systems
Technical Specifications
- Track System: Enclosed steel track with wheeled conveyor chain
- Support Structure: Self-supporting or suspended from structural steel
- Drive System: Electric gear motor (powered systems)
- Configurations: Straight, curved, vertical, and multi-level layouts
- Customization: Track layout, carriers, load capacity, and conveyor length tailored to client requirements
Applications
- Assembly and production lines
- Paint and coating systems
- Warehousing and distribution
- Automotive and industrial manufacturing
- Inspection, storage, and multi-floor material handling